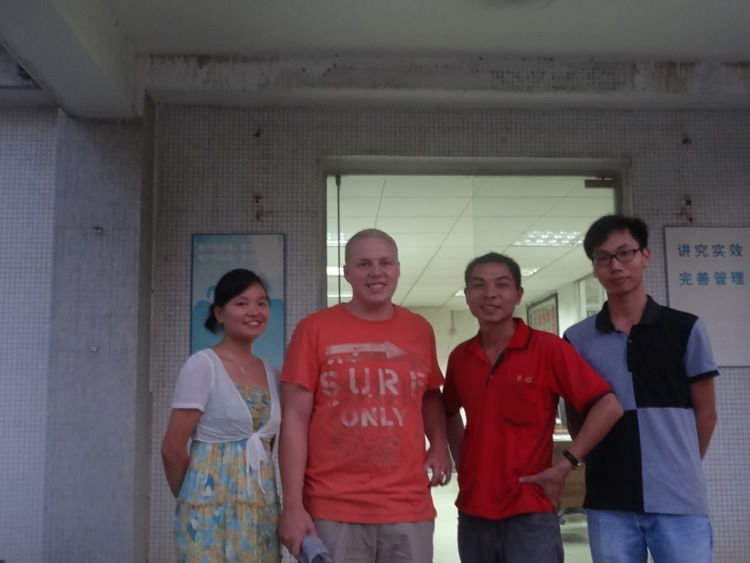
U.S. Client Visits Nuote Metals, Approves Tooling for Stamping Parts Project After On-Site Quality Audit
A U.S.-based OEM sourcing team concluded a two-day technical visit to Nuote Metals’ manufacturing facility in Dongguan last week, selecting the company as its tooling and production partner for a new stamping parts program. The decision followed a line-by-line review of Nuote Metals’ production floor and quality control system, with the client confirming that die development would proceed at Nuote Metals’ in-house tool room.
The visit began with a drawing and specification review, where the client’s engineering team walked through tolerance requirements, material callouts, and annual volume projections for the stamping parts family. Nuote Metals’ project engineers responded with a feasibility assessment covering strip layout, die progression, and press selection. The client then moved to the production floor, observing live runs on presses ranging from 25 to 200 tons—equipment used daily for steel, stainless steel, aluminum, brass, and copper stamping components.
Where the Quality Process Stood Out
The decisive part of the visit was the quality control walkthrough. Nuote Metals demonstrated three process controls that directly address the most common failure mode in stamped production: drift. Unlike a first-article-only inspection model, the company runs SPC on critical features, tracks tool wear by stroke count, and uses in-die gauging that stops the press before a stamping part drifts out of tolerance. The client reviewed live SPC charts, reviewed punch-face measurement records taken every 15,000 strokes, and observed die-temperature monitoring in operation. Nuote Metals maintains a Cpk target of ≥1.33 on production runs, with PPAP documentation available for programs that require it.
“What convinced us was not a certificate on the wall—it was seeing the process controls running at the press,” the client’s sourcing lead said during the closing session. “We have launched stamping parts programs where the first article passed and the batch drifted three weeks later. Nuote’s stroke-count tracking and in-die gauging give us confidence that the process is managed, not just sampled.”
The client also inspected incoming material verification—including coil-to-coil hardness checks before release to production—and reviewed a closed corrective-action file to assess how the supplier responds when a measurement exceeds its control limit. At the conclusion of the audit, the client confirmed that die design and fabrication would be placed with Nuote Metals, with first-article samples scheduled for review before mass production.
What This Means for Other Buyers Evaluating Stamping Parts Suppliers
Nuote Metals notes that the questions raised during this U.S. client visit mirror what most serious buyers ask before committing to a tooling investment. The company has published the following FAQ for sourcing teams at a similar stage.
FAQ: Sourcing Stamping Parts and Opening Tooling
1. How long does it take to develop a die for custom stamping parts?
Timelines depend on die type. Simple single-operation dies typically run 4–6 weeks; compound dies 6–8 weeks; progressive dies 10–14 weeks. Nuote Metals provides a milestone schedule covering design, fabrication, tryout, and first-article approval before a purchase order is issued.
2. What quality evidence can a buyer request before approving a stamping parts supplier?
At minimum: a recent PPAP or FAI package for comparable geometry, capability study data (Ppk on the initial run, ongoing Cpk), gage R&R results, and closed corrective-action records. On-site, buyers should verify that the control plan matches what is actually running at the press. Nuote Metals makes these records available during supplier audits.
3. Does every stamping parts project require IATF 16949?
No. ISO 9001:2015 remains the baseline for general industrial and commercial stamping parts. Automotive programs typically require IATF 16949 and PPAP submission. Nuote Metals aligns the quality documentation package with the end-use industry of the part.
4. What is the minimum order quantity for production stamping projects?
For production runs following tooling approval, Nuote Metals works from a minimum order quantity of 50,000 pieces on standard stamping parts programs. Prototype and sample quantities are handled separately before the production die is released.
5. When does opening a dedicated die make more sense than sourcing from existing tooling?
Dedicated tooling becomes the lower-cost path when annual volume is sufficient to amortize die construction and when the part geometry is stable enough to justify a production-intent process. Nuote Metals reviews volume, tolerance, and material with the buyer during the RFQ stage to recommend the appropriate tooling strategy.
About Nuote Metals
Nuote Metals is a Dongguan-based supplier of custom metal stamping parts for automotive, appliance, electronics, and electrical contact applications. Capabilities include in-house die design and fabrication, progressive and high-speed stamping, and PPAP documentation. The company works with steel, stainless steel, aluminum, brass, copper, and spring steel from 0.15 mm to 4.0 mm.
For sourcing teams planning a supplier visit or requesting a tooling review for a stamping parts program, Nuote Metals accepts drawing packages and specification files through its inquiry channel.
Send Inquiry
X
We use cookies to offer you a better browsing experience, analyze site traffic and personalize content. By using this site, you agree to our use of cookies.
Privacy Policy