What Separates a Reliable CNC Turning Service from a Quote-and-Ship Shop?
When Turning Is the Correct Process—and When It Is Not
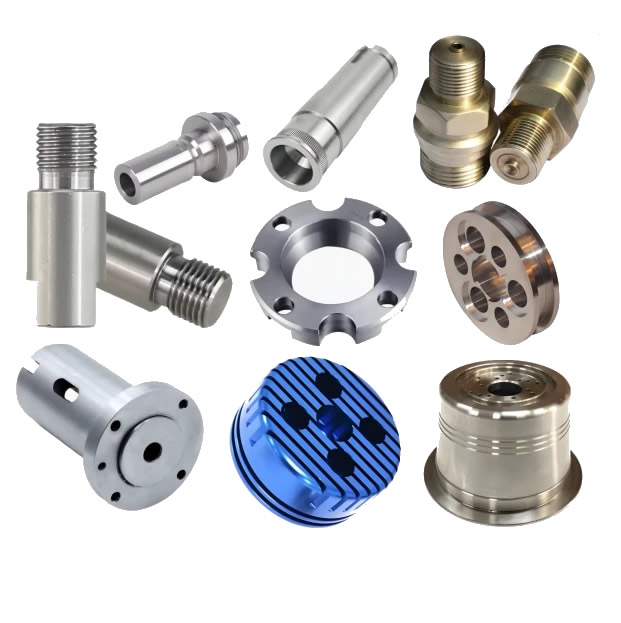
CNC turning is optimized for parts with symmetry along their center axis. A shaft dominated by OD and ID features will almost always be faster and cheaper to turn than to mill. Turned parts are typically produced faster and at lower cost than milled parts for round geometries.
Process Selection Matrix
| Part Geometry | Recommended Process | Reason |
|---|---|---|
| Shafts, pins, spacers, bushings | CNC turning | Rotational symmetry, continuous cutting action |
| Threaded connectors, fittings | CNC turning | OD/ID threads cut in single setup |
| Prismatic housings, pockets, multi-face features | CNC milling | Turning cannot reach features off the axis of rotation |
| Complex parts with both round and milled features | Mill-turn (5-axis) | Single clamping, no secondary operations |
A reliable CNC turning service will tell you when your part is not a turning job. If the critical features are pockets or hole patterns distributed across multiple faces, turning alone will require secondary operations that add cost and handling risk. The best suppliers flag this before quoting.
The Capability Signals That Actually Predict Performance
Machine lists and ISO certificates are starting points, not conclusions. What separates a capable CNC turning service from a marginal one is repeatability under production conditions.
Tolerance and Surface Finish—The Real Numbers
Capability Standard Range Precision Range What It Means for Your Part
| Capability | Standard Range | Precision Range | What It Means for Your Part |
|---|---|---|---|
| Dimensional tolerance | ±0.05 mm (ISO 2768-f) | ±0.005 mm to ±0.01 mm | Precision range requires ground clamping, thermal control, and in-process gauging |
| Surface finish (Ra) | 3.2 µm (as-machined) | 0.8 µm or better | Finer finishes require reduced feed rates, polished inserts, or secondary operations |
| Concentricity | 0.05 mm TIR | 0.01 mm TIR | Critical for mating shafts, bearing seats, and rotating assemblies |
ISO 2768-f for metals specifies ±0.05 mm on nominal sizes from 0.5 to 6 mm, and ±0.1 mm from 6 to 30 mm. A supplier claiming ±0.005 mm on a production basis should be able to show SPC data from a comparable part, not just a one-off sample.
The Swiss-Type Advantage for Slender Parts
For parts under 20–32 mm diameter with length-to-diameter ratios above 5:1, a sliding-headstock (Swiss-type) lathe is the correct equipment. The guide bushing supports the bar stock at the cutting zone, delivering substantially better vibration resistance than a fixed-head lathe. If your part is long and slender and the supplier quotes a fixed-head machine, expect deflection, chatter, or taper.
Quality Documentation—What a Serious Partner Provides as Standard
The difference between a capable CNC turning service and a transactional one is visible in the paperwork that ships with the parts.
First Article Inspection (FAI) Is Not Optional
FAI verifies that the first production part conforms to every drawing requirement. It is the baseline document for any new part introduction. For automotive programs, PPAP goes further—it demonstrates that the entire production system is repeatable, not just that one sample passed. A supplier that offers “dimensional reports on request” is telling you that FAI is an upsell, not a standard step.
In-Process Verification, Not Just Final Inspection
Final inspection catches defects after the value has already been added. A reliable turning partner verifies dimensions during production:
- CMM verification at first article, batch start, and final release
- Keyence or optical gauging for high-volume critical features
- SPC monitoring on tolerances that matter, with corrective action triggered by trend, not just out-of-spec
Material Traceability to the Heat Number
Every batch should trace back to the mill certificate for the raw bar stock. Without this, a material substitution or a heat-treatment inconsistency is invisible until the part fails.
Two Production Cases Where a Turning Change Solved the Problem
EV Motor Rotor Shaft (5-Axis Mill-Turn, Tolerance and Setup Reduction)
Problem: An electric vehicle motor supplier was producing rotor shafts across five separate turning and milling setups. Each re-clamping introduced concentricity error, and the cumulative stack-up pushed bore-to-OD runout beyond the ±0.02 mm limit. Scrap rate was 4%.
Our approach: We moved the part to a 5-axis mill-turn cell. Turning, milling, and drilling were completed in a single clamping. The elimination of re-clamping removed the primary source of concentricity error.
Result: Runout variation dropped below ±0.01 mm. Setup count fell from five to one, and scrap rate dropped below 0.5%.
Medical Bone Screw (Swiss Turning, Surface Finish and Traceability)
Problem: A medical device startup needed bone screws machined from 17-4PH stainless steel. The thread flanks required Ra below 0.8 µm for fatigue resistance, and every lot had to be traceable to the mill heat number. The previous supplier delivered parts that passed visual inspection but failed fatigue testing at the thread root.
Our approach: We machined the screws on Swiss-type lathes with live tooling for the drive feature. Threading was performed in a single continuous pass with a polished carbide insert, and Ra was verified on every 50th piece using a portable profilometer. Each lot shipped with the mill certificate and a dimensional report covering every drawing characteristic.
Result: Thread-root Ra measured consistently between 0.4 and 0.6 µm. Fatigue testing passed with margin. The customer eliminated 100% incoming inspection after the third lot.
Technical Specifications – Our Turning Envelope
| Parameter | Range | Notes |
|---|---|---|
| Max part diameter | 431 mm | Larger diameters require fixed-head lathes |
| Max part length | 990 mm | Longer parts may require special fixturing |
| Shank diameter tolerance | ±0.005 mm to ±0.05 mm | Precision range requires in-process gauging |
| Surface finish | Ra 0.4 µm to Ra 3.2 µm | Finer finishes available with secondary operations |
| Materials | Aluminum, brass, copper, stainless steel, carbon steel | Material-specific parameters apply |
For parts outside these ranges, we will tell you before quoting rather than after the first article fails.
FAQ
Q1: How do I know if my part should be turned or milled?
A: The decisive factor is geometry. If the part is rotationally symmetric—a shaft, pin, bushing, fitting, or connector—CNC turning is almost always faster and cheaper than milling. Turning uses continuous cutting action on a spinning workpiece, which yields higher material removal rates on round parts and lower tooling costs for medium to high volumes. If the critical features are pockets, slots, or hole patterns distributed across multiple faces, milling is the correct primary process. Parts that combine both round and prismatic features are best produced on a mill-turn center, which completes both operations in a single clamping. A capable CNC turning service will recommend milling when turning is not the right answer.
Q2: What quality documentation should I expect from a CNC turning service?
A: At minimum, demand First Article Inspection (FAI) on the first production part, a material certificate traceable to the mill heat number, and in-process inspection records for critical dimensions. For automotive programs, PPAP documentation is the standard—FAI alone does not demonstrate that the production system is repeatable. For medical or aerospace work, AS9102 (aerospace FAI) or ISO 13485-aligned process discipline may be required. A serious partner provides these as standard workflow steps, not as paid add-ons. If a supplier cannot show a completed FAI from a comparable part, the quality claim is unverified.
Q3: What tolerances can a CNC turning service realistically hold in production?
A: Standard production turning holds ±0.05 mm on metals per ISO 2768-f for nominal sizes under 30 mm. Precision turning routinely achieves ±0.01 mm with ground clamping and in-process gauging. Tolerances of ±0.005 mm are achievable on selected features with Swiss-type lathes and thermal compensation, but they require SPC monitoring—not just a one-time sample. The practical constraint is not the machine’s best-case capability but the supplier’s ability to hold that tolerance across thousands of parts. Ask for a control chart from a production run, not a single-part inspection report.
Q4: What is the MOQ and lead time for CNC turning at Nuote Metals?
A: Our standard MOQ is 500 pieces for custom turned parts, with lower quantities available for prototypes and first articles. Stock brass and standard connector profiles can ship from 100 pieces. Lead time for standard materials in production quantities up to 50,000 pieces is 7–12 days. Custom plating or secondary operations add 5–8 days. New parts requiring tooling and FAI allow 15–25 days total. Every quotation includes a firm lead time, not a range. ISO 9001:2015 certified.
Send Inquiry
X
We use cookies to offer you a better browsing experience, analyze site traffic and personalize content. By using this site, you agree to our use of cookies.
Privacy Policy